3D · HC102BV
Drag to rotate · pinch or use + / − to zoom
Inspect the lid, hinge or sliding drawer in normal use.
The source shows an independently larger inner tray from grooved rectangular stock. The post-machining foldable tray and its raw rectangular stock are both recorded. Its source tension coefficient is retained as a reference, separate from the full-caliper fit setting.
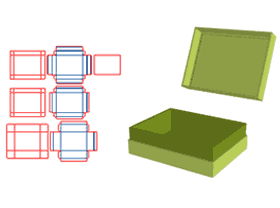
L/W are the main shell datum. H spans the shell floor/roof fold planes. Inside H measures the usable distance between material faces.
Complete closed assembly envelope: 202.4 × 152.4 × 63.2 mm
Inspect the lid, hinge or sliding drawer in normal use.
Outside artwork prints on wrapping paper. Inside artwork prints on lining paper. Greyboard remains a separate core.
Preview colours are separate from material caliper and print-ready colour specifications.
| Blank | Material | Caliper | Per set | Order blanks | Net area / set |
|---|---|---|---|---|---|
| Greyboard core | 2 mm | 1 | 100 | 0.0510 m² | |
| Outer wrapping paper | 0.2 mm | 1 | 100 | 0.0667 m² | |
| Greyboard core | 2 mm | 1 | 100 | 0.0510 m² | |
| Outer wrapping paper | 0.2 mm | 1 | 100 | 0.0759 m² | |
| Lining paper | 0.2 mm | 1 | 100 | 0.0291 m² | |
| Greyboard core | 2 mm | 1 | 100 | 0.0654 m² | |
| Outer wrapping paper | 0.2 mm | 1 | 100 | 0.0858 m² |
Net areas exclude holes and overlaps between panels in the same blank. Stock sheets, waste and adhesive are separate.
Different calipers have independent sheet plans. Each component remains a distinct blank. Prepared greyboard uses the full rectangular stock for sheet yield.
Sheet sizes are format references; the model uses 2 mm material. Confirm stock, grain and availability in the quotation.
All materials selected for SVG, DXF and OBJ. Animated glTF and the editable record contain the complete assembly.
The dieline shows the folding blanks after corner waste removal. Use Raw stock groove DXF for the rectangular board and extended groove axes.
The source shows an independently larger inner tray from grooved rectangular stock. The post-machining foldable tray and its raw rectangular stock are both recorded. Its source tension coefficient is retained as a reference, separate from the full-caliper fit setting. Source dimensions refer to the recorded studio plans. Fold-line width and assembled dimensions are related through the selected physical calipers and independent shell clearances. Cutter profiles, groove skin, adhesive build and final physical fit need confirmation on a production sample.
Packmage drawings, dimensions, options and accessible 3D states are recorded per design. EasyPackMaker provides independent construction-family and material-fit comparisons. Matching codes do not prove matching physical designs.
Tooling grooves, residual skin, adhesive compression, hardware and physical fit still require a supplier sample. This is an independently editable construction, with source-specific differences recorded; factory equivalence is not claimed.